How to Choose an Injection Mold Manufacturer in 2026?

Choosing an injection mold manufacturer in 2026 requires more than comparing quotations. A supplier may promise speed, precision, and low costs. The real test appears later, when steel, resin, tolerances, and production pressure meet.

John Bozzelli, founder of RJG, puts it plainly: “The mold is the heart of the injection molding process.” His observation remains practical. A well-designed mold can stabilize cycle times, reduce defects, and protect long-term production costs. A poor one may create flash, warpage, short shots, and repeated maintenance work.

This guide examines how to evaluate injection mold manufacturing partners with evidence, not impressive claims. It considers engineering experience, material knowledge, mold-flow analysis, machining capability, inspection equipment, and trial documentation. It also reviews communication practices, project transparency, after-sales support, and the manufacturer’s ability to manage design changes.

Look beyond the initial price. Ask for comparable case studies, sample inspection reports, and clear acceptance criteria. Confirm whether the supplier understands your resin, annual volume, product tolerances, and intended machine conditions. A factory producing simple consumer parts may struggle with medical, automotive, or high-temperature applications.

Digital monitoring and sustainable production matter in 2026. Yet technology alone does not guarantee dependable tooling. Skilled engineers still interpret data, question assumptions, and correct problems before steel is cut.

No checklist is perfect. I have seen attractive proposals hide weak maintenance planning. That is why this article also addresses uncomfortable warning signs, including vague timelines, unexplained cost reductions, and resistance to design reviews. The best partner is not always the cheapest. It is the manufacturer that can repeatedly prove its decisions.
How to Choose an Injection Mold Manufacturer in 2026?

Define Your Injection Mold Requirements and Production Goals

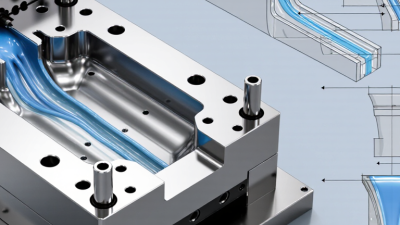
Choosing an injection mold manufacturer starts with a precise production brief, not a low quotation. Describe the part’s length, wall thickness, draft angles, undercuts, surface finish, and critical tolerances. State the resin grade, color, expected annual volume, target cycle time, and required mold life. Include the molding machine’s platen size, clamp force, nozzle position, and available controls. Small omissions become expensive changes. An experienced manufacturer should review these details through documented design-for-manufacturing feedback. Ask for a manufacturability review before steel is cut.

Production goals should be measurable. Define acceptable scrap rates, inspection frequency, sampling standards, and delivery milestones. For tight tolerances, request a realistic capability discussion supported by measurement records or trial data. Confirm whether the quotation includes mold-flow analysis, prototype testing, dimensional reports, and corrective iterations. Clarify hot-runner needs, ejection strategy, cooling layout, and spare-wear components. These choices affect cycle stability and maintenance costs. Do not treat a polished presentation as proof of capability. Ask who controls revisions and how approval decisions are recorded.

In one project, I focused too heavily on the initial unit price. The mold met the drawing, yet cooling was uneven near a thick boss. Cycle times drifted, and operators adjusted settings manually. That experience changed my evaluation method. I now compare tool design, trial discipline, communication, and after-sales response alongside price. Request references for similar materials and part geometries, then verify what support was actually delivered. A reliable partner welcomes difficult questions and records changes openly. I still sometimes underestimate approval time, so I build contingency into the schedule.

How to Choose an Injection Mold Manufacturer in 2026?

Define Your Injection Mold Requirements and Production Goals

Mold life should be matched to the expected production volume. These industry planning benchmarks help buyers compare prototype, bridge-production, and full-production tooling requirements before selecting a manufacturer.

Prototype tooling Suitable for design validation and early functional testing, typically up to about 10,000 molding cycles.
Bridge-production tooling Useful for pilot runs and market testing, commonly planned for approximately 10,000–100,000 cycles.
Production tooling Designed for repeat manufacturing, with a typical planning target of 100,000 to 1,000,000 or more cycles.

Use these ranges as planning references rather than guarantees. Actual mold life depends on resin type, part geometry, steel selection, maintenance, cycle time, and operating conditions.

Assess Manufacturer Expertise, Equipment, and Quality Systems

Choosing an injection mold manufacturer in 2026 requires more than comparing hourly rates. Assess experience with your resin, part geometry, tolerances, and expected annual volume. Ask for anonymized case evidence, mold-flow studies, cycle-time records, and examples of corrective actions. A supplier should explain why a gate, cooling layout, or ejection method was selected. Vague answers are warning signs.

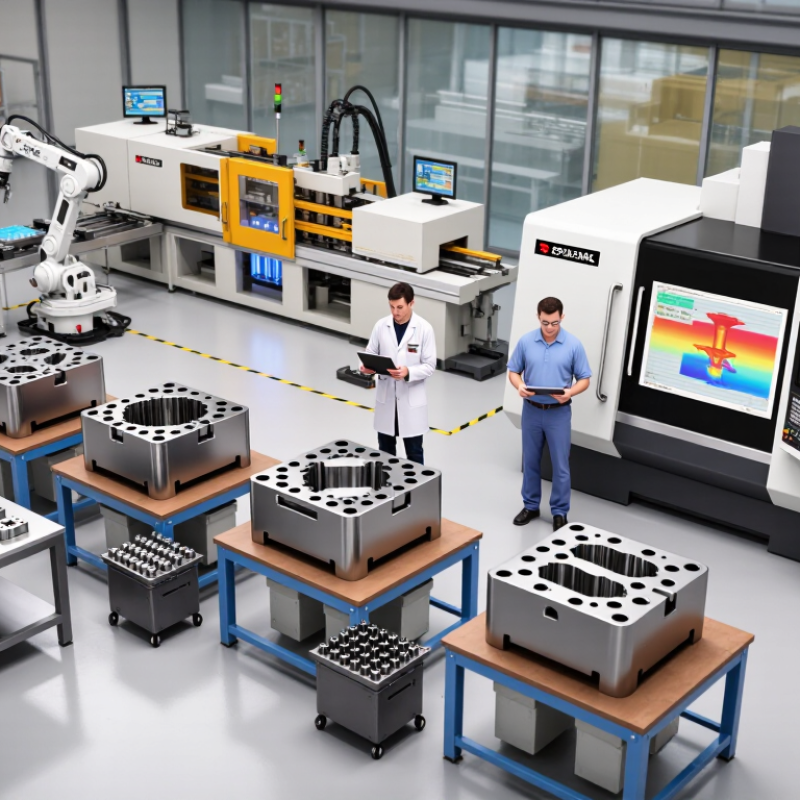
Inspect the equipment directly. Check press size, shot capacity, injection repeatability, mold-temperature control, and preventive-maintenance records. Confirm that measurement tools are calibrated and that the factory can measure critical dimensions after molding. Modern equipment helps, but it cannot repair weak process knowledge. Deloitte’s 2024 Global Smart Manufacturing Survey found that 86% of manufacturing leaders expect smart manufacturing to drive competitiveness within five years. Yet automation without disciplined data collection can produce faster defects. That point is easy to overlook.

Quality systems deserve equal attention. The ISO Survey 2023 reported more than 1.2 million ISO 9001 certificates worldwide, but certification alone proves limited daily performance. Request process-control plans, inspection sampling rules, material traceability, nonconformance logs, and CAPA records. For regulated or safety-critical parts, review validation protocols and change-control procedures. Walk through one real batch record. Look for resin lot numbers, machine settings, operator checks, and final inspection results. No audit is perfect. I would still question suppliers that display certificates prominently but cannot show recent defect trends. Performance data matters more than polished paperwork.

Compare Tooling Processes, Materials, Costs, and Lead Times

How to Choose an Injection Mold Manufacturer in 2026?
Compare Tooling Processes, Materials, Costs, and Lead Times

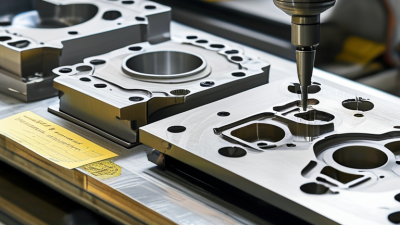
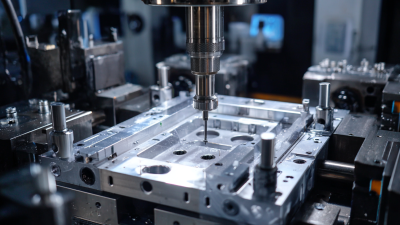
When evaluating an injection mold manufacturer, compare the tooling process against your expected production volume. CNC machining suits many standard molds and offers predictable accuracy. Electrical discharge machining helps create deep ribs, sharp corners, and hardened steel details. Additive tooling can reduce development time, but surface finish and service life may vary. It is useful for prototypes, not every production program.

Material selection changes both cost and lead time. P20 steel often balances machining effort, durability, and price for moderate production. Hardened tool steel costs more, yet it can withstand demanding cycles and abrasive materials. Aluminum molds may deliver parts quickly, but they usually offer shorter service life. Ask how the manufacturer handles cooling channels, ejector wear, and resin shrinkage. Small design mistakes become expensive after steel cutting begins.

Request a cost breakdown, not only a total figure. Separate mold design, machining, polishing, testing, modifications, and freight. A low quote may exclude trial shots or correction work. Not always. Confirm the promised lead time with a written production schedule and inspection points. My own early estimates sometimes ignored revision time. That was a costly lesson. A capable supplier should provide dimensional reports, material certificates, sample approval records, and clear change-control procedures. Judge communication during quoting, too. Slow answers before the order rarely improve afterward.

How to Choose an Injection Mold Manufacturer in 2026?
Compare Tooling Processes, Materials, Costs, and Lead Times

Tooling Process / Mold Type Typical Mold Material Recommended Production Volume Typical Tool Life Typical Tooling Cost (USD) Typical Lead Time Dimensional Capability Best-Fit Applications Main Advantages Main Limitations
Prototype Mold Aluminum, soft steel, or modular mold inserts 1–10,000 parts Approximately 500–20,000 shots $3,000–$25,000 2–6 weeks Generally suitable for prototype and early design validation; final tolerance depends on design and machining quality Design verification Market testing Low-volume parts Low initial investment, fast iteration, and convenient design changes Limited service life, lower wear resistance, and usually unsuitable for long-term mass production
Aluminum Production Mold 7075 or similar high-strength aluminum alloy; steel inserts may be added in wear areas Up to approximately 50,000–100,000 parts, depending on resin and geometry Approximately 10,000–100,000 shots $5,000–$35,000 3–8 weeks Good dimensional accuracy and fast heat transfer; less stable than hardened steel for long production runs Short runs Consumer products Non-abrasive resins Fast machining, lower tooling cost, lightweight construction, and shorter cooling cycles Lower resistance to abrasion, corrosion, and high clamping or injection loads
Soft Steel Mold Pre-hardened P20 or equivalent mold steel Approximately 50,000–500,000 parts Approximately 100,000–500,000 shots $15,000–$60,000 6–12 weeks Good production-grade accuracy when properly machined, fitted, and tested General production Medium volumes ABS and PP parts Balanced cost, machinability, strength, and maintainability Shorter life than hardened steel and less suitable for highly abrasive or corrosive materials
Hardened Steel Mold H13, 1.2311/1.2312, S136, or comparable hardened tool steel 500,000–2,000,000+ parts Approximately 500,000–2,000,000+ shots with suitable maintenance $30,000–$150,000+ 10–20 weeks High dimensional stability and repeatability for demanding production environments High-volume production Tight tolerances Abrasive resins Long service life, excellent wear resistance, and strong process consistency Higher machining, heat-treatment, polishing, and maintenance costs; longer manufacturing time
Stainless Steel Mold 420 stainless steel, S136, or similar corrosion-resistant mold steel 100,000–1,000,000+ parts Approximately 300,000–1,500,000+ shots $35,000–$160,000+ 12–22 weeks High surface quality and good dimensional stability, especially in humid or corrosive environments Medical components Optical surfaces Corrosive resins Excellent corrosion resistance, polishability, cleanliness, and long-term repeatability Higher material and machining costs; specialized heat treatment and polishing may be required
Family Mold P20, H13, S136, or a combination selected for the required tool life Usually medium to high volume, with multiple related parts per cycle Determined by the selected steel and the most wear-sensitive cavity $25,000–$150,000+ 10–20 weeks Each cavity can be accurate, but filling and cooling balance between different parts is critical Product assemblies Related components Cost-sensitive programs Produces several related components in one cycle and can reduce machine time and handling Complex mold balancing, unequal cavity filling, different shrinkage behavior, and more difficult quality control
Multi-Cavity Mold Usually P20 for moderate volume or hardened steel for high volume 100,000 to several million parts Approximately 500,000–2,000,000+ shots, depending on construction $40,000–$250,000+ 12–24 weeks High repeatability is achievable when cavity, cooling, and runner balance are controlled High-volume identical parts Automotive components Consumer goods Lower per-part tooling allocation, high output, and efficient machine utilization High upfront cost, complex balancing, longer validation, and expensive repairs if multiple cavities are affected
Hot Runner Mold Hardened or pre-hardened steel with hot runner components and wear-resistant inserts Typically 250,000 to several million parts Approximately 500,000–2,000,000+ shots with proper maintenance $50,000–$300,000+ 14–26 weeks Good repeatability and reduced material variation when temperature control is properly tuned High-volume production Thin-wall parts Reduced scrap requirements Eliminates or reduces cold runners, lowers material waste, and supports faster automated cycles Higher initial cost, more complex maintenance, greater sensitivity to contamination, and more difficult troubleshooting
Insert-Molding Tool Tool steel with replaceable cores, slides, lifters, and hardened wear inserts 10,000–1,000,000+ parts Depends on insert material, loading method, and production handling $20,000–$180,000+ 8–20 weeks Requires accurate control of insert location, retention, resin flow, and operator or automation repeatability Metal inserts Electrical parts Mechanical assemblies Combines molding and assembly, reduces secondary operations, and can improve component integration More complex loading, increased risk of insert displacement, and higher validation requirements
Overmolding Tool P20, H13, S136, or corrosion-resistant steel selected for the substrate and resin combination 50,000–1,000,000+ parts Determined by the mold steel, substrate design, and number of molding stages $30,000–$180,000+ 10–22 weeks Requires control of substrate location, bond area, shrinkage, flash, and interface dimensions Soft-touch products Seals and grips Two-material components Integrates multiple materials, improves ergonomics, and reduces assembly operations More difficult mold design, material compatibility risks, and higher process-validation effort
Typical 2026 planning ranges for conventional injection molds. Actual results vary with part size, number of cavities, resin, tolerances, surface finish, automation, cooling design, validation requirements, and geographic labor rates.
Selection guidance: Choose aluminum or prototype tooling for design validation and limited quantities; pre-hardened steel for balanced medium-volume production; hardened or stainless steel for long service life, abrasive or corrosive materials, and tight tolerances; and multi-cavity or hot-runner tooling when high output and lower unit cost justify the higher initial investment.

Verify Communication, Compliance, Capacity, and Supplier Reliability

How to Choose an Injection Mold Manufacturer in 2026?

Choosing an injection mold manufacturer in 2026 requires evidence, not polished presentations. Start with communication. Ask for a named project owner, response-time targets, and weekly tooling updates. Request one design review covering cavity layout, cooling channels, draft angles, and molding risks. Short answers can expose weak engineering discipline. So can silence.

A practical test is a controlled change request. Send a revised tolerance or resin requirement, then record clarification speed and document accuracy. It resembles production, not sales theater. We often overvalue fluent English; that is a mistake. Clear drawings, revision control, and escalation paths matter more. Verify compliance at the facility, not through a certificate scan. The ISO Survey 2023 recorded 1,265,216 valid ISO 9001 certificates worldwide. Certification is widespread, but not automatically sufficient. Audit traceability for steel, resin, inspections, and corrective actions. Ask for anonymized records.

Capacity needs numbers. Request machine tonnage, mold-size limits, available shifts, maintenance schedules, inspection equipment, and current loading. Compare promised output with cycle time, cavitation, scrap rate, and downtime. “Unlimited capacity” is fog. Validate claims with a pilot mold and staged ramp plan. Review delivery performance, defect rates, financial continuity, backup utilities, and subcontractor controls. The World Manufacturing Forum’s 2024 report emphasizes resilient, digitally visible production. Yet visibility can remain partial. Supplier audits may miss hidden dependencies. Plan contingency tooling, transparent milestones, and a realistic second source.

Evaluate Prototypes, Contracts, Support, and Long-Term Partnership Value

How to Choose an Injection Mold Manufacturer in 2026?

A reliable evaluation starts with the prototype, not the sales presentation. Ask for a molded sample using your real resin, wall thickness, and draft angles. Inspect flash, sink marks, weld lines, and parting-line accuracy under strong light. Request dimensional reports with actual measurement data, not general assurances. A capable manufacturer should explain what failed during trials and how the tooling was adjusted. That honesty matters.

Contracts deserve equal attention. Define steel grades, mold ownership, revision limits, acceptance standards, delivery milestones, and maintenance duties. Include a clear process for engineering changes. Ambiguous clauses can create expensive arguments later. I have seen promising projects slow down because “approved sample” had no measurable definition. That mistake is preventable.

Support after delivery often separates a vendor from a long-term partner. Ask how quickly they respond to tooling wear, short shots, or inconsistent cycle times. Confirm spare-part availability, preventive maintenance records, and technical communication channels. A useful partner studies production data before suggesting changes. They should also protect your drawings and process information through appropriate confidentiality controls. Do not judge partnership value by the lowest quotation alone. Compare response quality, trial discipline, and problem-solving depth. The cheapest mold may become costly after six months. Even strong suppliers can miss a detail. Regular reviews keep assumptions visible and encourage better decisions.

NEW JERSEY

Location

Union Tool & Mold is a mold making, repair and plastic injection molding company located in central New Jersey.
(973) 763-6611

220 Rutgers St, Maplewood, NJ 07040
ACCREDITED

Certified Company


SOCIAL PROFILE

Let’s Connect

We invite you to engage with us on LinkedIn, where you can stay updated on our latest news, insights, and professional opportunities.